Explore equipment, consumables and technical specifications for industrial procurement. Select your requirements and request a quotation.
Carbon & Low-Alloy Steel Electrodes
Reference configuration — confirm the required execution when enquiring.
One source-specific SMAW operating row; current range applies only to the stated diameter and length. Match base metal, joint and qualified welding procedure before quotation. Packaging and availability require confirmation. The manufacturer reports a modified E6018 classification; this is not an unmodified E6018 reference.
- AWS classification
- E6018 (mod.)
- AWS specification
- A5.1 / SFA-5.1
- EN ISO classification
- 2560-A: E 35 4 B 4 2 H5
Request a quotation →
Carbon & Low-Alloy Steel Electrodes
Reference configuration — confirm the required execution when enquiring.
One source-specific SMAW operating row; current range applies only to the stated diameter and length. Match base metal, joint and qualified welding procedure before quotation. Packaging and availability require confirmation. The manufacturer reports a modified E6018 classification; this is not an unmodified E6018 reference.
- AWS classification
- E6018 (mod.)
- AWS specification
- A5.1 / SFA-5.1
- EN ISO classification
- 2560-A: E 35 4 B 4 2 H5
Request a quotation →
Carbon & Low-Alloy Steel Electrodes
Reference configuration — confirm the required execution when enquiring.
One source-specific SMAW operating row; current range applies only to the stated diameter and length. Match base metal, joint and qualified welding procedure before quotation. Packaging and availability require confirmation. The manufacturer reports a modified E6018 classification; this is not an unmodified E6018 reference.
- AWS classification
- E6018 (mod.)
- AWS specification
- A5.1 / SFA-5.1
- EN ISO classification
- 2560-A: E 35 4 B 4 2 H5
Request a quotation →
Carbon & Low-Alloy Steel Electrodes
Reference configuration — confirm the required execution when enquiring.
One documented SMAW configuration. Verify base-metal grade, welding procedure and supply pack before quotation. Published current or gas information applies to this reference only.
- AWS classification
- E7018-1 H4R
- AWS specification
- A5.1 / SFA-5.1
- EN ISO classification
- 2560-A: E 42 5 B 4 2 H5
Request a quotation →
Carbon & Low-Alloy Steel Electrodes
Reference configuration — confirm the required execution when enquiring.
One documented SMAW configuration. Verify base-metal grade, welding procedure and supply pack before quotation. Published current or gas information applies to this reference only.
- AWS classification
- E7018-1 H4R
- AWS specification
- A5.1 / SFA-5.1
- EN ISO classification
- 2560-A: E 42 5 B 4 2 H5
Request a quotation →
Carbon & Low-Alloy Steel Electrodes
Reference configuration — confirm the required execution when enquiring.
One documented SMAW configuration. Verify base-metal grade, welding procedure and supply pack before quotation. Published current or gas information applies to this reference only.
- AWS classification
- E7018-1 H4R
- AWS specification
- A5.1 / SFA-5.1
- EN ISO classification
- 2560-A: E 42 5 B 4 2 H5
Request a quotation →
Carbon & Low-Alloy Steel Electrodes
Reference configuration — confirm the required execution when enquiring.
One documented SMAW configuration. Verify base-metal grade, welding procedure and supply pack before quotation. Published current or gas information applies to this reference only.
- AWS classification
- E7018-1 H4R
- AWS specification
- A5.1 / SFA-5.1
- EN ISO classification
- 2560-A: E 42 5 B 4 2 H5
Request a quotation →
Carbon & Low-Alloy Steel Electrodes
Reference configuration — confirm the required execution when enquiring.
One documented SMAW configuration. Verify base-metal grade, welding procedure and supply pack before quotation. Published current or gas information applies to this reference only.
- AWS classification
- E7018-1 H4R
- AWS specification
- A5.1 / SFA-5.1
- EN ISO classification
- 2560-A: E 42 5 B 4 2 H5
Request a quotation →
Carbon & Low-Alloy Steel Electrodes
Reference configuration — confirm the required execution when enquiring.
One documented SMAW configuration. Verify base-metal grade, welding procedure and supply pack before quotation. Published current or gas information applies to this reference only.
- AWS classification
- E7018-1 H4R
- AWS specification
- A5.1 / SFA-5.1
- EN ISO classification
- 2560-A: E 42 5 B 4 2 H5
Request a quotation →
Carbon & Low-Alloy Steel Electrodes
Reference configuration — confirm the required execution when enquiring.
One documented SMAW configuration. Verify base-metal grade, welding procedure and supply pack before quotation. Published current or gas information applies to this reference only.
- AWS classification
- E7018-1 H4R
- AWS specification
- A5.1 / SFA-5.1
- EN ISO classification
- 2560-A: E 42 5 B 4 2 H5
Request a quotation →
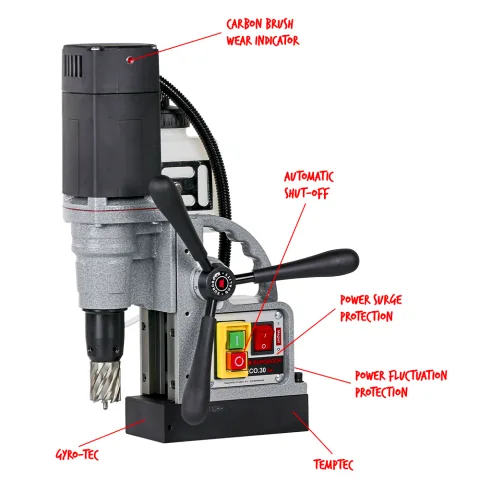
Retained source illustration. Model candidate illustration; exact execution and configuration are not approved.
Magnetic Drilling Machines
Source-backed reference
ECO.30S+ is a Euroboor magnetic drilling machine for annular cutting up to 30 mm. Its 19.05 mm Weldon spindle supports the separately stated drilling and countersinking tools. Choose the supply execution, cutter, pilot pin and lubrication for the workpiece and required hole.
- Annular cutting
- 12–30 mm diameterAnnular cutter capability only; tool, workpiece and drilling conditions require selection.
- Twist drilling / countersinking
- Twist 1–13 mm; countersinking 10–35 mm diameterSeparate tool operations; no tapping capacity inferred.
- Stroke / spindle
- 90 mm stroke; 19.05 mm Weldon spindleExact source model; tool projection and usable working space require confirmation.
Request a quotation →
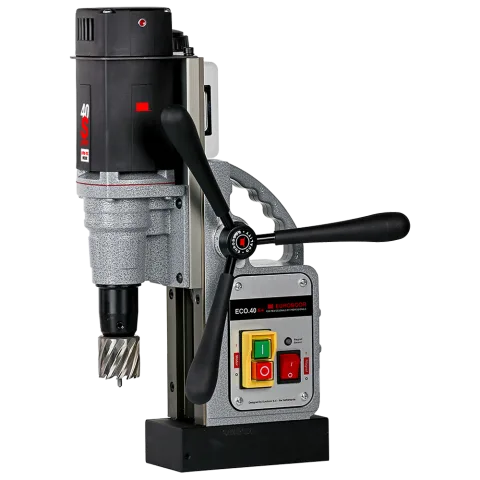
Retained source illustration. Model candidate illustration; exact execution and configuration are not approved.
Magnetic Drilling Machines
Source-backed reference
ECO.40S+ is a Euroboor magnetic drilling machine for annular cutting up to 40 mm. Its 19.05 mm Weldon spindle supports the separately stated drilling and countersinking tools. Choose the supply execution, cutter, pilot pin and lubrication for the workpiece and required hole.
- Annular cutting
- 12–40 mm diameterAnnular cutter capability only; tool, workpiece and drilling conditions require selection.
- Twist drilling / countersinking
- Twist 1–16 mm; countersinking 10–45 mm diameterSeparate tool operations; no tapping capacity inferred.
- Stroke / spindle
- 145 mm stroke; 19.05 mm Weldon spindleExact source model; tool projection and usable working space require confirmation.
Request a quotation →
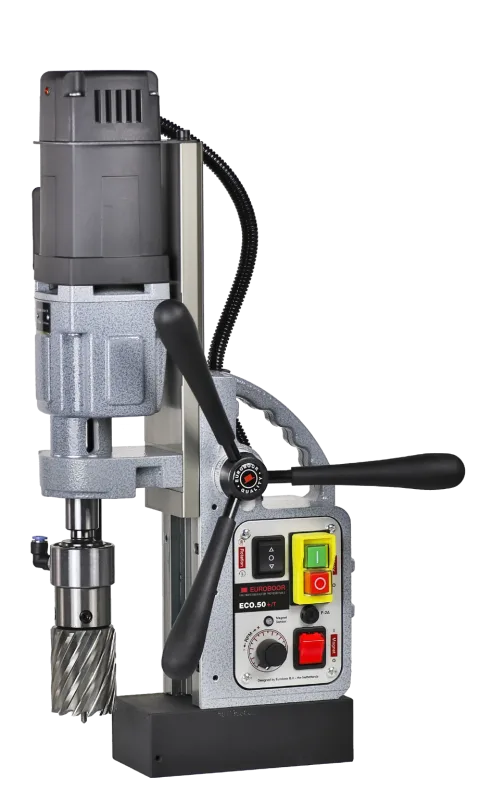
Retained source illustration. Model candidate illustration; exact execution and configuration are not approved.
Magnetic Drilling Machines
Source-backed reference
Euroboor ECO.50+/t is a magnetic drilling machine for annular cutting, twist drilling, countersinking and tapping. Choose the documented voltage/frequency execution and matching tooling before quotation; its drilling capacities describe different operations rather than one interchangeable limit.
- Annular cutting
- 12–50 mm diameterExact ECO.50+/t operation and stated loaded/no-load basis; selected power execution applies.
- Twist drilling
- 1–23 mm diameterExact ECO.50+/t operation and stated loaded/no-load basis; selected power execution applies.
- Countersinking
- 10–55 mm diameterExact ECO.50+/t operation and stated loaded/no-load basis; selected power execution applies.
Request a quotation →
Copper-Nickel Welding Electrodes
Reference configuration — confirm the required execution when enquiring.
Copper-base 70/30 copper-nickel joining and surfacing; specify the exact base alloy and qualified procedure. Published current and polarity apply only to this diameter/length reference. Confirm the base-metal grade, qualified procedure and supply pack before quotation.
- AWS classification
- ECuNi
- AWS specification
- A5.6 / SFA-5.6
- Process
- SMAW
Request a quotation →
Copper-Nickel Welding Electrodes
Reference configuration — confirm the required execution when enquiring.
Copper-base 70/30 copper-nickel joining and surfacing; specify the exact base alloy and qualified procedure. Published current and polarity apply only to this diameter/length reference. Confirm the base-metal grade, qualified procedure and supply pack before quotation.
- AWS classification
- ECuNi
- AWS specification
- A5.6 / SFA-5.6
- Process
- SMAW
Request a quotation →
Copper-Nickel Welding Electrodes
Reference configuration — confirm the required execution when enquiring.
Copper-base 70/30 copper-nickel joining and surfacing; specify the exact base alloy and qualified procedure. Published current and polarity apply only to this diameter/length reference. Confirm the base-metal grade, qualified procedure and supply pack before quotation.
- AWS classification
- ECuNi
- AWS specification
- A5.6 / SFA-5.6
- Process
- SMAW
Request a quotation →
Hardfacing Electrodes
Reference configuration — confirm the required execution when enquiring.
Reference coated-electrode size and recommended current. Hardness is a typical all-weld as-welded property, not a guaranteed hardness on every substrate or layer. Pack mass/piece count are shown only for the exact sizes listed in the source.
- Electrode classification
- EN 14700: E Fe 8
- Form
- Basic-coated stick electrode for hardfacing
- Nominal analysis (wt%)
- C 0.5%; Si 2.3%; Mn 0.4%; Cr 9.0%; Fe balance
Request a quotation →
Hardfacing Electrodes
Reference configuration — confirm the required execution when enquiring.
Reference coated-electrode size and recommended current. Hardness is a typical all-weld as-welded property, not a guaranteed hardness on every substrate or layer. Pack mass/piece count are shown only for the exact sizes listed in the source.
- Electrode classification
- EN 14700: E Fe 8
- Form
- Basic-coated stick electrode for hardfacing
- Nominal analysis (wt%)
- C 0.5%; Si 2.3%; Mn 0.4%; Cr 9.0%; Fe balance
Request a quotation →
Hardfacing Electrodes
Reference configuration — confirm the required execution when enquiring.
Reference coated-electrode size and recommended current. Hardness is a typical all-weld as-welded property, not a guaranteed hardness on every substrate or layer. Pack mass/piece count are shown only for the exact sizes listed in the source.
- Electrode classification
- EN 14700: E Fe 8
- Form
- Basic-coated stick electrode for hardfacing
- Nominal analysis (wt%)
- C 0.5%; Si 2.3%; Mn 0.4%; Cr 9.0%; Fe balance
Request a quotation →
Hardfacing Electrodes
Reference configuration — confirm the required execution when enquiring.
Reference coated-electrode size and recommended current. Hardness is a typical all-weld as-welded property, not a guaranteed hardness on every substrate or layer. Pack mass/piece count are shown only for the exact sizes listed in the source.
- Electrode classification
- EN 14700: E Fe 8
- Form
- Basic-coated stick electrode for hardfacing
- Nominal analysis (wt%)
- C 0.5%; Si 2.3%; Mn 0.4%; Cr 9.0%; Fe balance
Request a quotation →
Submerged Arc Welding Wires
Reference configuration — confirm the required execution when enquiring.
Reference wire classification and diameter from the identified source sheet. Weld-metal properties depend on the exact wire/flux combination and qualified welding procedure. No spool mass, welding-current range or interchangeable flux is inferred; confirm the supplied execution at quotation.
- Process
- SAW
- Form
- Copper-coated solid wire
- Wire classification
- EH10
Request a quotation →
Submerged Arc Welding Wires
Reference configuration — confirm the required execution when enquiring.
Reference wire classification and diameter from the identified source sheet. Weld-metal properties depend on the exact wire/flux combination and qualified welding procedure. No spool mass, welding-current range or interchangeable flux is inferred; confirm the supplied execution at quotation.
- Process
- SAW
- Form
- Copper-coated solid wire
- Wire classification
- EH10
Request a quotation →
Submerged Arc Welding Wires
Reference configuration — confirm the required execution when enquiring.
Reference wire classification and diameter from the identified source sheet. Weld-metal properties depend on the exact wire/flux combination and qualified welding procedure. No spool mass, welding-current range or interchangeable flux is inferred; confirm the supplied execution at quotation.
- Process
- SAW
- Form
- Copper-coated solid wire
- Wire classification
- EH10
Request a quotation →
Submerged Arc Welding Wires
Reference configuration — confirm the required execution when enquiring.
Reference wire classification and diameter from the identified source sheet. Weld-metal properties depend on the exact wire/flux combination and qualified welding procedure. No spool mass, welding-current range or interchangeable flux is inferred; confirm the supplied execution at quotation.
- Process
- SAW
- Form
- Copper-coated solid wire
- Wire classification
- EH12K
Request a quotation →